Showing posts with label Stress. Show all posts

Wednesday, 16 September 2026

Wreaths

Can glass wreaths be made from bottles?

Last autumn a small group within the cooperative Jangling Space decided to see if we could make strip construction glass wreaths for Christmas.  This developed out of a collaborative project with Christopher Jeffree on whether bottle glass could be made to fit together at various sizes of frit.

Testing for compatibility of glass at frit levels

It was postulated that small sized frits did not allow stress to build to critical length beyond the frit size.  Work is still going on to discover the upper limits to the frit size for this postulation to become invalid.

We speculated that the same brand bottles from the same drinks manufacturer would be compatible.  We thought this possible, because there are few bottle manufacturers that can produce the number of bottles required and that they would have consistency.  After some experiments with same colour wine bottles we found very inconsistent compatibility.  But some volume wine producers use distinctive bottle colours, which seem to have consistency.

After some experimentation we settled on green Gordons gin bottles combined with blue bottles of a reueda wine bottled under the Four Lines brand, both of which had consistency between bottles and production runs and showed acceptable stress levels between them for these purposes. This was important to be able to distinguish by colour the stress between the frit particles. The microscopic investigation of these frit combinations did show incompatibilities, but at very short lengths.  The stress between less compatible frits was indeed interrupted by the connection of groups of wholly compatible ones.  This was successfully tested in various proportions (25%, 50%, 75%) and sizes from 75 microns to 1200 microns. Testing for larger frits remains to be conducted.

Producing the flat glass

Jangling Space had been producing sheet glass from bottles by analogy from hand blown glass — where the glass cylinder has the ends cut off, and then split — for several years.  After experimentation, it was found that cutting out a quarter of the bottle cylinder, the largest piece of flat glass could be made.  Of course, we tended toward brighter greens, yellow greens, pale ambers, and various shades of blue. This kept part of the glass pallet inexpensively supplied. 

Experimenting for the wreaths

A group of four gathered together to conduct the experimentation and preparing for a wreath making class.  Knowing that the Gordons green bottles were consistently compatible, whether as retail or bar sized bottles enabled progress toward using strips to combine into fused objects. 

 Strips were decided upon because:

  • it is simple to provide parts for people with no fusing knowledge or experience to assemble,  

  • there is less waste than from shards piled on top of one another,

  • consistent widths of strips placed on edge would make annealing more accurate,

  • It would provide a distinctive wreath pattern

We began experimenting with size, arrangement, paints, glues, Frits, glass dots, etc., to provide stability, texture, decoration.


The first element was to establish the principle, so began with small wreaths of about 15cm/6”.  These were quick to assemble on shelf paper and we tried sticking them together with CMC.  This was messy and required significant drying time before they could be moved.  The second assembly test was to use frit to stabilise the pieces.  We found we could use thin but relatively stiff plastic sheets to move the pieces on shelf paper to the kiln with little disturbance.

The pieces were fired at a 200°C/360°F rate to 720°C/1328°F for 10 minutes. This temperature was chosen as it is the softening temperature for float glass, which we believed would be enough to stick the glass together without loosing the textures of the radiating strips.  We did not use the double thickness for scheduling and annealing as is usual in unevenly thick projects.  Instead the pieces were annealed as for 12mm/0.5” although the strips averaged just less than 10mm, but of course there were gaps to be considered.


They came out looking well, and with acceptable levels of stress.  But they proved to be fragile when handled. Inspection showed that the wreaths were breaking where the attachment points were small.  This led to heaping fine and medium frit over the strips – rather than fitting fine frit between – for the next set of wreaths.  It was also felt that the wreaths were pretty dark, so we decided to add clear glass from Gordons gin bottles in a ratio of two green strips to one clear strip. At the same time some of the wreaths had some Bullseye red and white dots added to add more colour.  These were fired to 740°C/1364°F. There was little difference in texture of the strips – only a little more rounding – but the frits were more like sand than an enhancement to the wreath.  We also found that the clear bottle glass increased the amount of stress, so we went back to all green.  The dots showed very little stress, so they became part of the assembly.  

Again, although more robust in handling, they were still fragile.

Having learned

  • frit can stabilise the unfired strips

  • frits need to be medium to large for a good appearance

  • higher temperatures are required

  • only the green Gordons glass could be used

  • Small Bullseye dots could be sparsely spread over wreaths

We went to a larger scale – 28cm/11”.

Stepping up in scale required a lot more glass – we found two bottles were needed to provide enough strips for a wreath.  That is a lot of 75mm/3“ strips! We produced a lot of quenched frit from the bottle necks and bottoms, which required a lot of pounding and sifting, to get rid of the fine and powdered glass.  At this scale drawing the limits for the strips became important to maintain the circular doughnut form.  Props were needed to keep the strips upright, as many of the cuts were not clean, due to the thickness variations caused by the embossing of the Gordons design on each bottle.


The essential "sprinkling" of coarse frit for a couple of centimetres (ca. 1”) out from from the centre of the strips was about two layers thick.  During the firing most of this sank into the voids between the ends of the strips, and left a "moraine" texture over the internal part of the wreath.  It gave an impression of the strips flowing out from the centre, or possibly as a retreating glacier.  It provided strength to the vulnerable/weak areas where the sides of the strips contact each other.


This increase in size needed radiating guide lines to keep the strips radiating from the centre, rather than bunching up side by side.   More short pieces were needed to fill outer gaps than expected from the smaller trials. The increased size required not only more glass, but a more robust method of transferring the unfired pieces to the kiln.  A couple of things were investigated until we discovered pizza shovels.  This was ideal to slide under the shelf paper and carefully carry to the kiln.  Also more storage space was needed, as not all the wreaths could be fitted into the kiln at once. The minor problems of scale!.

A contour fuse was used to

  • maintain a lot of the undulations of the glass,

  • allow some bending over to lower pieces, and

  • make better contacts and incorporation of the pieces.

These fired well giving a much more robust, although heavy, wreath that was admired by the group and the members of Jangling Space. This reveal of what the group had been doing led to the suggestion of stringing LED lights and ribbons around the wreaths.

In preparation for the hands-on making of wreaths by members of Jangling Space, it was decided to make “statement” wreaths of 38cm/15” diameter.   A trial showed that three large Gordons bottles would be required to make them.  Also an additional 50% more frit required to be made.

Jangling Space members had to provide and clean sufficient bottles.  They were cut and flattened for them, and frit made from the necks and bottoms.  Each person had to cut their own strips after being shown that breaking thick glass is easier with cut running pliers without cushions.  They assembled and decorated their wreaths and the experimental group placed the frit around the inner part of the wreath.  The results were placed on a large pizza shovel and transferred to the kiln, and the waiting ones to storage shelves.


For the class that was subsequently offered, the bottles were provided by Jangling Space members who helped clean them.  Members of the experimenting group cut, flattened, cut strips, made frit and red and white balls so each class attender had a set of parts with which to assemble their wreaths. It went surprisingly well.

Thanks to Chris, Linda, Lyndsey and all the others who helped in this project.

Wednesday, 29 July 2026

Frit Stretch Crack


Description

A frit stretch in the flattening developed two internal cracks at 4:00 and 8:00 going through colours (but not felt on top or bottom). The flattening was to reduce the centre thickness from about 8m, to be nearer the 6mm of the edges. It was fired in a side element kiln. The maker does not know if there is stress beyond the cracks.

The question is about firing again to conceal the cracks.

Schedules first.

Generally side fired kilns need to have up ramp rates for at least one thickness greater than top fired kilns to counteract uneven heating. The heat input to glass with side fired kilns is directly to the edge of the glass and so more uneven than in top fired kilns. Slower rates for the up ramps are needed than for top firied kilns. Down ramps are not affected in the same way, so down rates can be the same as for top fired kilns.

1st firing (before the break):

277°C/500°F – 594°C/1100°F, 0’ [A reasonable first ramp for small pieces]

28°C/50°F – 691°C/1275°F, 60’ [At 691°C the glass has begun to stick together, so a lower temperature of 677°C/1250°F would continue to allow air out as the glass slumped.]

9999 – 830°C/1525°F, 60’ [This speed allowed only about 15 minutes to get to top temperature. The impossibility of the glass equalising the top to bottom temperature is alleviated by the one hour soak. The hotter top layers of the stretch begin to move toward the centre before the bottom layers. This ASAP 3rd segment will reduce the time for the flow to the centre. Peeking at intervals will show when, or if, the centre has been filled by the flow.]

9999 – 510°C/950°F, 120’ [It is known a frit stretch will have a variation in thickness from about 9mm to 6mm. This would indicate firing for at least 1.5 times the thickest part, approximately 12mm, which is what was done]

28°C/50°F – 427°C/800°F, 0’ [A two hour soak indicates annealing for 12mm, so the cooling needs to be for that too. 55°C/100°F to 427°C/800°F is adequate. And can be followed by 99°C/180°F to 371°C/700°F. The final cool rate could be as fast as 330°C/600°F to room temperature.]

Off

If there are no more than 5 segments available in the kiln controller, use the slower first rate to 371°C/700°F. If the natural cooling rate of your kiln is more than the slow first rate at that temperature, reduce the target temperature further.

I rarely fire faster than 330C/600F to top temperature. Faster does not allow all the heat to reach the bottom and so meld the glass together. There are two blog posts that help to explain the difficulties with AFAP ramps up in temperature. This difference increases with thickness. The effects on glass temperatures, and the heat control problems


2nd firing:

111°C/200°F – 594°C/1100°F, 0’ [because of the cracks, I suggest 55°C/100°F is fast enough as the first ramp rate. But it does not need to go to more than 500°C/932°F to be sure of being above the strain point.]

125°C/225°F – 663°C/1225°F, 30’. [I would maintain this rate to top temperature, as any bubbles are already trapped]

9999 – 830°C/1525°F, 60’ [I would use this top temperature and time but at the slower rate of the previous ramp]

9999 – 510°C/950°F, 120’ [I think this is an appropriate anneal soak time]

28°C/50°F – 427°C/800°F, 0’ [The cool rate should be as suggested for the first firing. The elimination of the bubble squeeze segment allows a final segment rate of 100°C/180°F – 371°C/700°F or lower if required – for a controller with fewer segments.]


You need to put the heat into the glass slowly when trying to flatten or thin a piece. With a slow rate it may be possible to reduce the one hour soak at top temperature and still get the same thinning result.

The break goes through colours so it is not a compatibility problem. That moves attention to annealing soak and cooling. The schedules do not set off any alarms for me as causing the crack (although I would have been more cautious). It is clearly highly stressed with the crack essentially going across the whole piece except the edges. It will continue to be delicate because of the stress unless re-fired carefully.

Testing for stress

A stress test is a means of determining how sound the fired piece is. It can also be used on smaller pieces to determine what stresses may be stored in the glass and to determine if the glasses are compatible.

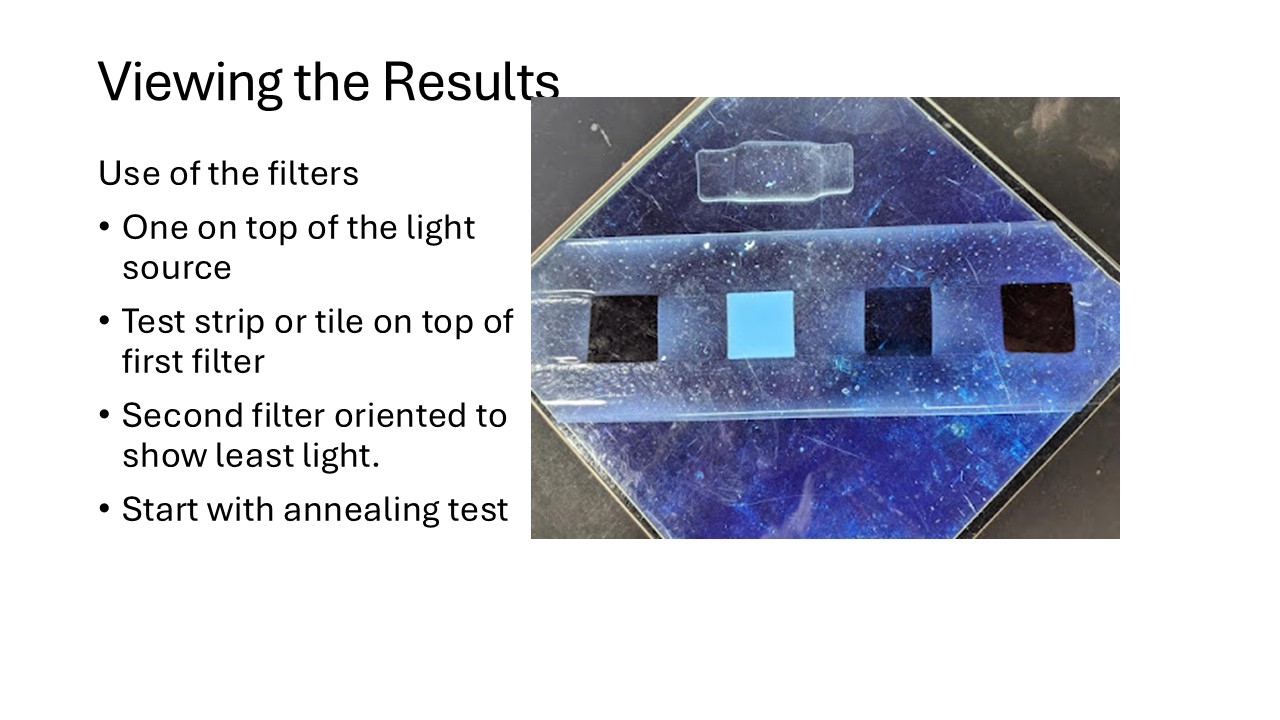
This tests for both stress and compatibility.  These give notes on the use of the polarised filters.

Strain Point

The strain point is the temperature above which the viscosity of the glass is low enough that it is rarely subject to thermal shock, because it is no longer brittle. That temperature is determined by the glass’s viscosity, which is achieved at different temperatures for different glass, such as float glass.

Repair

I suggest placing a dam around the piece before firing for a repair. This can be thick fibre paper backed with kiln furniture, or some other circular material to confine the piece, in case the crack develops into a full break during the firing.

The Ramp Rate I suggested of 55°C/100°F per hour is because of the existing cracks. This is to avoid inducing additional stress to the piece during the temperature increase. Once the strain point is passed, the rate can be increased. I suggest the rest of the firing should be as for 12mm / 0.5". The anneal soak and cooling are given in the Bullseye document Annealing Thick Slabs, Celsius and  Fahrenheit,  which is applicable to "CoE 96" glasses, except for the anneal soak temperature.

Further investigation

I suggest two e-books which will be very helpful in your exploration of kilnforming:

Kilnforming Principles and Practices, by Stephen Richard

Firing Schedules for Kilnformed Glass, by Bob Leatherbarrow

Both are available from Bullseye or the authors.

Wednesday, 25 March 2026

Relieving Existing Stress - How?

Why is the stress not relieved after the strain point when slumping?


The answer relates to whether it is on the cool or on the heat up.

Cooling

The annealing occurs at a higher temperature than the strain point. The aim of the annealing soak is to even out the temperature within the glass to be equal to or less than 5°C/10°F (∆T=5C). When this small differential in temperature is achieved, there is little stress in the glass. In an adequate anneal, stress will be relieved during the soak. This differential needs to be maintained through the first cool, taking the glass temperature to below the strain point.

Relieving stress occurs between the glass transition point to just above the strain point. The viscosity of the glass is so high below the strain point (brittle phase) of the glass that no stress can be relieved.

The more rapid cooling during the brittle phase of the glass needs to be slow enough to avoid creating large contraction differentials within the glass. The reason for progressive cooling stages during the brittle phase of the glass is that it can withstand greater temperature differentials and so the cooling rates can be increased.

Heat up

Any stress on the way up for an already fused piece is induced by uneven heating. This can be across the piece, which is most evident in side fired kilns. The source of the infrared heating is nearest the edge of the glass, so it heats first leaving the centre cooler – sometimes the difference in expansion is great enough to break the glass.

In top fired kilns the differential is usually between top and bottom surfaces. Glass transmits heat slowly so the difference in temperature between the top and the bottom can be enough to cause a break from unequal expansions.

Both these conditions are caused by rapid ramp rates and short anneals on the cool.

Ramp Rates

Breaking of a flat piece on the kiln shelf is from too short a soak or too fast a cool, or both (unless there is an incompatibility). Breaking in a slump most often is a result of too rapid an initial ramp rate. A fused piece needs slower ramp up rates in a slump than in the initial fuse. It is now a single thicker piece, rather than multiple pieces as at the beginning of a fuse. While you might fire a flat 6mm/0.25” piece at 200°C/360°F for the fuse, the ramp rate for the slump needs to be no more than about 100°C/180°F. Tack fused pieces need much slower heat up rates during the slump, usually only half of the rate used to fuse the piece.

Tests have shown that even though the anneal soak for both firings can be the same, a more stress-free piece can be achieved by annealing as for one layer thicker. I do not know why, but I speculate that it is more difficult to achieve the ∆T=5C in the curved piece, than in a flat one.


More information is available in the ebook Annealing Concepts Principles and Practice.


Wednesday, 18 March 2026

The Relationship of Stress and Slumping

From time to time the assertion is that a break during the heat up of a blank while slumping is the result of residual stress remaining in an under-annealed blank.  Is there a relationship between inadequate annealing and slumping breaks?

It seems to be the general consensus that it is true.

It is clear that poorly annealed glass is more likely to break.  The assumption is that the additional bending stress added to the existing stress, causes a break.  Even if the fused piece is stressed, but not enough to break, a slow heat up would avoid the build up of stress to breaking level.  After all, the means of relieving the stress of toughened/tempered glass is by a slow heat up to allow the stress between the interior and surface to be equalised.  The same principle should apply to stressed glass in a slump.  My contention is that the ramp rates for the slump have been too fast to relieve any additional stress applied by the bending of the glass.

I hear of very few people testing for stress after any firing.  I read of people asserting the existing stress is amplified on the slump firing.  I do not read of any experience of people testing their flat piece, discovering excess stress, and  re-firing to relieve the stress before slumping, but the assertion of excess stress from the first firing continues as a cause.

Without testing there is no way to know whether the first firing had excessive stress.  The use of polarising filters is such a simple, easy and quick way to determine if there are stress problems in the fired and cooled piece.  It should be the business of practitioners and teachers to assert the need for stress testing as the next task when the glass has cooled. Unless people asserting this possibility do the testing of their proposition, it can only remain among the untested elements of kilnforming.

If there were to be a lot of stress in the flat blank, it needs to be fired again, annealed longer and cooled more slowly than previously to relieve the stress before any other process is conducted.  The firing to relieve the stress needs to be only to the lower portion of the slumping range at maximum.  

Each piece that is intended for further firing, needs to be tested for stress before the next firing, and not just at the end of the firing sequence.  To get an accurate reading of the stress, the piece must be allowed to cool until the internal temperature equals the surface temperature.  This may take overnight, but at least as long as the combined anneal soak and the associated cool. The delay caused by waiting for the complete cool may encourage people to skip the stress testing.  But it is risky to avoid testing for stress because of impatience.  Another firing can be conducted while waiting for the first piece to completely cool.

Annealing sufficiently on every firing is the way to ensure that any slumping break is not the consequence of stress from the previous firing.  The Bullseye sheet Annealing Thick Slabs (Celsius and Fahrenheit) gives the annealing times and cool rates.  This document applies to all fusing glass, except the annealing temperature used. Study the table, and follow it closely.  Keep in mind that the effective thickness for other than full fuse, is between 1.5 to 2.5 times the thickest part.  After that first firing, test the piece for stress when it has cooled sufficiently.  It is also important to test the successfully slumped piece for stress before using, gifting, or selling it.


Wednesday, 21 January 2026

Stress Testing - How?


 This is a presentation I gave a while ago on why and how to test for stress without risking the piece, that is, non-destructive testing.


Wednesday, 8 October 2025

How Can I Relieve Stress in Fused Glass?

An stress test strip and annealing witness between polarised filters.

If an unbroken fired piece shows stress that is known not to be from incompatibility, it is possible to fire and anneal again to relieve the stress.  If the stress results from incompatibilities, annealing again will not change the compatibility.  The process for stress testing is here. 

Conditions for doing this re-firing are:

  • Slower heat up rates than usual for this thickness and profile are required. The glass is more than usually fragile and needs gradual heating. This avoids creating additional stress that may cause a break.

  • Take the temperature up to the lower end of slumping temperature range - say 600 - 620C (1100 - 1150F) - and soak for 10 – 30 minutes depending on profile and thickness.  This ensures any existing stress is relieved and the glass is ready for the annealing.

  • Reduce the temperature as fast as possible to the existing or new annealing temperature.

  • Anneal for longer than previously. This can be for a greater thicknesses than the thickness and profile used for the stressed piece.  Most importantly, the anneal soak for the combination of profile and thickness needs to be followed.

  • My experimentation has shown that the profile determines the additional amount of thickness that needs to be allowed for a sound anneal is as follows:

    • Full flat fuse - fire for the thickness (i.e. times 1)
    • Contour fuse -  fire for 1.5 times the thickest part
    • Rounded tack fuse - fire for 2 times the thickest part
    • Sharp tack/sinter - fire for 2.5 times the thickest part.
  • Use the cool rates related to the anneal soak time. These are available from the Bullseye site for Celsius and Fahrenheit.  Too rapid a cool can induce temporary stress from differential contraction of the glass that is great enough to cause breaks, so follow the rates determined for this thickness and profile. 

  • These rates are scientifically determined for all glass and especially for fusing glass and are inversely related to the anneal soak.  That means the longer the anneal soak, the slower the cooling rates need to be, and directly related to the soak length.  It does not matter which manufacturer's glass is being used, all the target times and temperatures should be followed, except the annealing temperature.


More information is available in my e-book Annealing Concepts, Principles, and Practice available from Bullseye, Etsy, and stephen.richard43@gmail.com

Wednesday, 16 April 2025

Testing for Stress

Testing for stress is one of the most important elements in kilnforming.  It may not look like there is stress when there is considerable amounts.  The non-destructive tests are outlined in this Power Point presentation, prepared some time ago, to describe why and how stress testing can be conducted.  There is no commentary.